Is Your CMM Costing You More Than It Should?
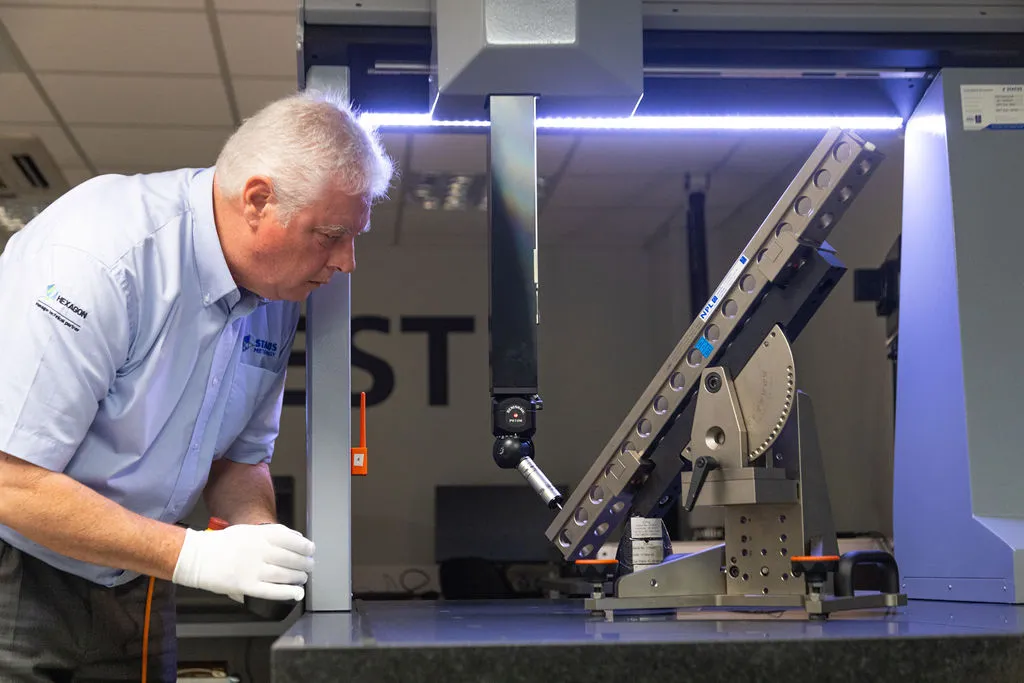
A CMM does not have to be broken to be costing your business money.
If parts are queuing for inspection, programming is tying the machine up, faults are becoming more frequent or production is regularly waiting for results, it is worth looking at whether the current setup is working as efficiently as it could be.
Sometimes the issue is the machine. Sometimes it is the way the inspection process is working around it.
Either way, it is always worth understanding where time is being spent and whether your inspection process is running as efficiently as it could be.
Start with the Bottleneck
If parts are regularly queuing for inspection, look at what the CMM is actually doing.
Is it measuring for most of the shift, or is a lot of time being used for programming, setup and proving new routines? Are jobs waiting because only one person knows how to run them? Is every component going through the CMM because that is simply how it has always been done?
If demand has genuinely outgrown the available capacity, another CMM may well be the right answer.
But if the machine is spending too much time doing work that could be handled differently, there may be easier gains to make first.
Keep the CMM Measuring
Programming directly on the machine makes sense for some work, especially one-off components.
The problem comes when programming starts taking up valuable inspection time.
Offline programming allows programmes to be prepared away from the CMM so the machine can keep measuring while the next job is being developed.
If programming is regularly competing with inspection for machine time, that can make a noticeable difference.
Does Every Part Really Need the CMM?
A fixed CMM is still the right tool for a huge amount of dimensional inspection, but that does not mean every inspection job needs to go through it.
For example, large fabrications, installed assemblies or awkward components may be better suited to portable measurement. Portable measuring arms can support probing and 3D scanning for work such as first article inspection, tooling checks, assembly verification and reverse engineering.
For manufacturers that do not have this capability in-house, we can also provide portable inspection at your premises where moving the component would be difficult or disruptive. This can help free up the fixed CMM for the work that really needs it.
The same principle applies to subcontract inspection. If there is a temporary spike in workload, a major project or a machine outage, outsourcing some work can be a practical way to stop a backlog building.
Repeated Faults Have a Cost Beyond the Repair
The repair itself is only part of the cost. If the CMM is down, inspection can stop, first-off approvals can be delayed and production can quickly start backing up.
If faults are becoming more frequent or the same machine is regularly causing disruption, it is worth reviewing whether the current maintenance approach still suits the way the CMM is being used.
Do Not Write Off a Good Machine Because It Is Old
If an older CMM is starting to cost more to maintain, replacing it might seem like the obvious next step. But age alone does not tell you whether a machine still has plenty of useful life left in it.
A CMM can remain mechanically sound long after controllers, software and probing systems have moved on. In those cases, an upgrade or retrofit may extend the useful life of the machine without replacing the whole system.
On the other hand, there comes a point where the application itself has changed. The components may be larger, tolerances tighter, volumes higher or parts and support harder to get.
At that stage, a new or refurbished CMM may be the better long-term option.
The key question is whether the machine is still right for the work you need it to do.
Are You Getting Enough From the People and Software You Already Have?
Of course, the CMM itself is only part of the inspection process. How it is programmed and used day to day can have just as much impact on efficiency.
If an experienced programmer is constantly correcting programmes, operators are repeating avoidable steps or the team relies on one person for every difficult job, throughput will suffer.
That is where training can have a real operational benefit. The aim is not just to make people faster. It is to help them build reliable inspection routines, use the software properly and deal with problems without unnecessary trial and error.
Five Questions Worth Asking
If you want to understand how efficiently your CMM and wider inspection process are working, these five questions are a good place to start:
- How much of the working day is the CMM actually measuring?
- How often is production waiting for inspection results?
- How much machine time is spent programming, setup or proving routines?
- Are repeated faults or support issues affecting planned work?
- Is every job being measured on the CMM because it needs to be, or because that is the established process?
Even if everything is working well, these are useful questions to revisit from time to time.
Small inefficiencies can creep into any inspection process as workloads change, new parts are introduced or different people start using the equipment.
Keeping an eye on where time is being spent can help you spot opportunities to improve efficiency before they become a bigger issue.
That might mean maintenance, training, offline programming, portable inspection, subcontract support, an upgrade, extra CMM capacity or a different machine altogether.
Status Metrology supports CMMs throughout their working life, from servicing, software and training through to portable measurement, subcontract inspection, upgrades and new or refurbished machines.
If you want a second opinion on how efficiently your current inspection setup is working, get in touch and our team will be happy to help.
Frequently asked questions
Our Proud Partners



 +44 (0) 1159 392 228